6 Mandatory Processes for Galvanized Wire to Reach 2-Year Service Life for Marine Aquaculture Cages
Release time:
2026-08-06
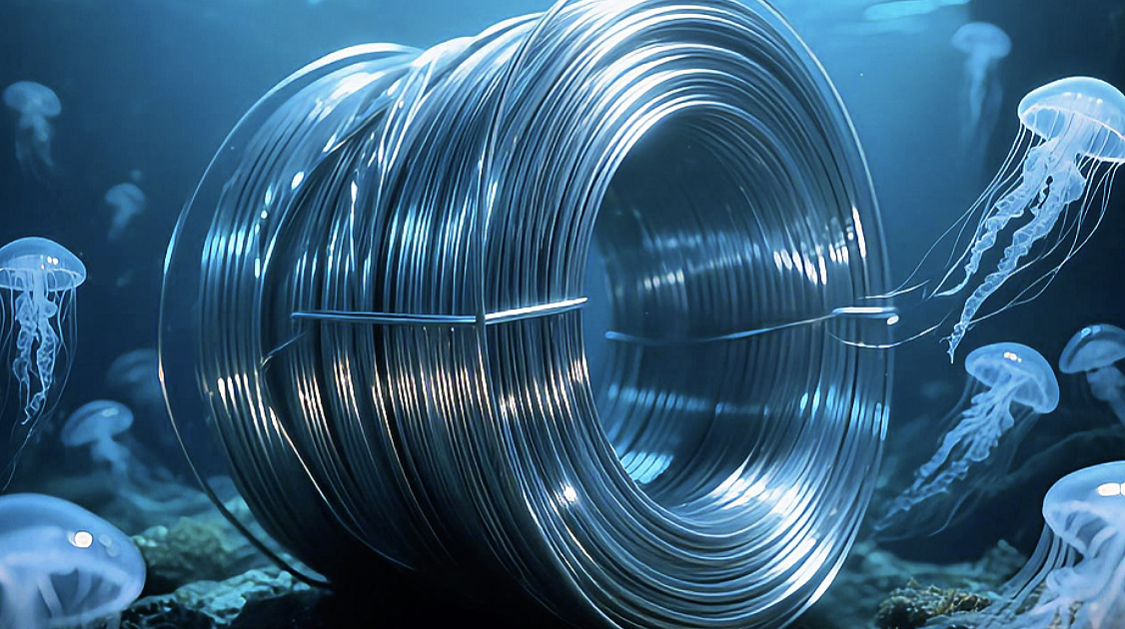
Seawater features high chloride concentration, alternating wet-dry cycles, marine organism adhesion and structural bending stress, bringing severe electrochemical corrosion to cage binding galvanized wire.
Introduction
Seawater features high chloride concentration, alternating wet-dry cycles, marine organism adhesion and structural bending stress, bringing severe electrochemical corrosion to cage binding galvanized wire. Ordinary cost-cutting galvanized wire will develop severe white rust, coating peeling and brittle fracture within 6–10 months. To achieve a stable service life of 2 years for marine aquaculture cages, six core production processes cannot be omitted or simplified.
1. Constant-Temperature Continuous Annealing for Base Steel Wire
Process Requirement
Adopt through-type constant-temperature continuous annealing furnace to fully release internal tensile stress of drawn steel wire, uniform metal grain structure.
Core Function
Prevent zinc coating cracking when twisting, binding and cage forming. Simple intermittent annealing wire retains massive internal stress; tiny cracks will form on the galvanized layer after bending, allowing seawater chloride ions to invade rapidly and cause perforated corrosion.
Prohibition Rule
Reject low-cost simple annealed wire.
2. Full Pre-Galvanizing Pretreatment System
Three-step standardized pretreatment is the premise of void-free galvanization:
- High-temperature alkaline degreasing to remove drawing lubricant and surface grease;
- Inhibitor-acid pickling to eliminate iron oxide scale, avoid over-pickling induced steel hydrogen embrittlement;
- Even flux coating + hot air drying.
Core Function
Eliminate bare steel spots, skip plating and zinc nodules. Even a tiny exposed steel point will turn into a deep corrosion pit under seawater erosion.
3. Matte Hot-Dip Galvanization (Electro-Galvanized Bright Wire Forbidden)
Key Technical Indicators
- Zinc bath constant temperature controlled at 440–460℃ to form three-layer compact zinc-iron alloy metallurgical bonding layer;
- Minimum zinc coating weight: ≥300g/㎡;
- Adopt gradient slow cooling, ban direct cold water quenching (rapid cooling creates countless microcracks on zinc coating).
Upgrade Option for Deep Sea
Galfan coating (5% aluminum-zinc alloy hot dipping), 35% higher chloride corrosion resistance than pure zinc coating.
Reminder
Mirror-bright electro-galvanized wire only has 10–30g/㎡ thin zinc coating without alloy bonding layer, which will pulverize and rust within 5 months in seawater.
4. Trivalent Chromium Passivation after Galvanizing
Process Standard
Conduct environmental trivalent chromium passivation immediately after galvanizing cooling; hexavalent chromium passivation is prohibited for aquaculture projects due to toxicity limits.
Core Function
Form an inert conversion film on the zinc surface, reduce the electrochemical activity of zinc, slow down the rapid generation of loose white rust. White rust cannot provide anti-corrosion protection and will continuously consume the zinc sacrificial layer. Passivation doubles the salt spray resistance of bare galvanized wire.
5. Silane Sealing Treatment (Decisive Process for Seawater Condition)
Process Standard
Immerse the passivated wire in silane sealing agent for full coverage and curing drying.
Core Function
Fill all micropores and microcracks on the passivation film to build a secondary physical barrier against salt fog and moisture. It also resists abrasion from seashells and algae attachment.
Measured Data
Galvanized wire with 300g/㎡ zinc coating without sealing fails in 12 months at sea; wire with passivation + silane sealing steadily serves more than 24 months.
6. Finished Product Protection & Standard Construction Operation
Factory End
Dry warehouse storage for finished wire, avoid outdoor damp stacking to prevent early white rust before installation.
Construction End Specification
- One-time bending & binding, prohibit repeated sharp twisting to avoid coating rupture;
- Use rubber/plastic gaskets for isolation when contacting copper, stainless steel and other dissimilar metals, block galvanic corrosion;
- Clean attached shellfish and algae on cages every 6–8 months to eliminate local concentrated salt corrosion caused by water retention of attachments.
Conclusion
Only galvanized wire equipped with constant-temperature annealing base wire, complete pretreatment, thick matte hot-dip zinc coating, gradient slow cooling, trivalent chromium passivation and silane sealing can satisfy the 2-year anti-corrosion demand for marine aquaculture cages. Any simplified process will directly cut the service life in half and bring extra maintenance and cage replacement losses for fish farmers.

Keywords:
More information


Contact
Phone/WhatsApp:
E-mail:
Address:
Huangtai Industrial Park, Xiaozhan Town,
Jinnan District, Tianjin, 300353, China
Follow us

Inquiry